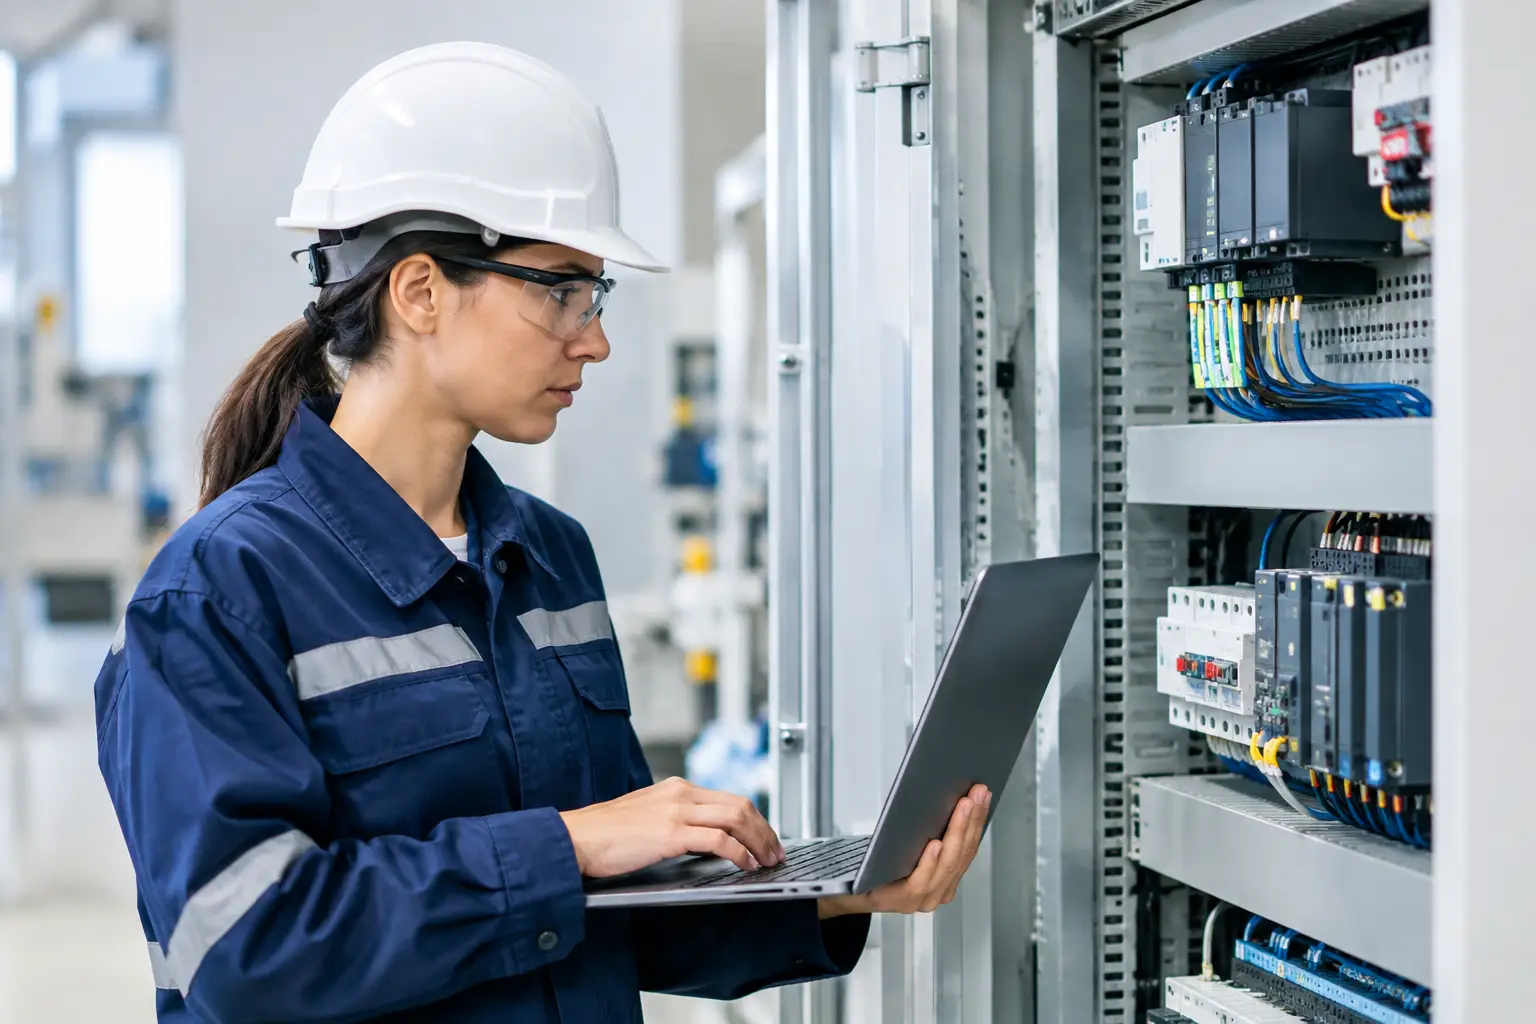
A production line stops because one sensor reports an impossible value. A pump trips at the wrong pressure. An operator can see an alarm but cannot tell what caused it. These are the practical problems a controls engineer is hired to prevent, diagnose, and improve.
The role sits where physical equipment, electrical systems, software, and plant operations meet. Controls engineers make machines and processes behave predictably. Their work may be largely invisible when a facility is running well, but it becomes immediately visible when uptime, quality, safety, or throughput starts to slip.
What a Controls Engineer Owns
A controls engineer designs, programs, tests, and supports the systems that automate equipment. In a manufacturing plant, that may mean coordinating conveyors, robots, vision systems, motors, and packaging equipment. In water treatment, energy, food processing, or chemical facilities, it can mean controlling flow, temperature, pressure, level, and other process variables.
The exact scope depends on the industry and employer. Some controls engineers spend most of their time developing new machine controls. Others support an existing facility, troubleshoot failures, and plan upgrades during short maintenance windows. System integrators often move between customer sites, while engineers in a large plant may become deeply familiar with one process over many years.
At the center of the job is a simple question: what should this system do under normal conditions, and what should it do when conditions are not normal? The answer has to be translated into hardware, logic, operator screens, alarms, and documentation that people can use under pressure.
A typical project begins with requirements. The engineer may review process descriptions, electrical drawings, equipment specifications, and safety expectations. From there, they select or work with selected hardware such as programmable logic controllers, remote I/O, variable frequency drives, sensors, actuators, safety relays, and industrial networks.
Programming is only one part of the work. A PLC program can be logically correct and still fail in the field because a wire is landed on the wrong terminal, a sensor is poorly placed, a drive parameter is incorrect, or the process itself behaves differently than expected. Good controls work connects software decisions to real equipment behavior.
From Signals to Decisions
Most automated systems follow a loop. Inputs tell the controller what is happening. The controller applies logic. Outputs command equipment to respond. A photoelectric sensor may detect a carton, a PLC may decide when it has reached the correct position, and an output may trigger a pneumatic cylinder to divert it.
That sounds straightforward until real-world conditions arrive. Sensors get dirty. Motors draw more current as equipment wears. Products vary slightly in size. Network communication drops out. Operators need manual control for maintenance but should not be able to create an unsafe sequence.
Controls engineers account for these conditions through interlocks, timers, permissives, fault handling, and clear operating modes. An interlock prevents an action when a required condition is absent. A permissive allows an action only after related equipment is ready. Those distinctions matter because they affect how operators understand a fault and how quickly a machine can safely return to service.
For process control, the engineer may use a PID loop to hold a variable near a target. A temperature controller, for example, compares the measured temperature with a setpoint and adjusts heating or cooling output. Tuning that loop is not a matter of selecting one universal setting. A slow-moving tank, a fast heating element, and a system with transport delay each require a different approach.
The Tools Behind Industrial Automation
Controls engineers work across several technical layers. PLCs handle deterministic machine and process logic. Human-machine interfaces, or HMIs, give operators status, alarms, trends, and commands. Supervisory control and data acquisition systems, commonly called SCADA, can collect data and supervise larger groups of equipment.
Common programming languages include ladder logic, structured text, function block diagrams, and sequential function charts. Ladder logic remains widely used because maintenance teams can often read it quickly. Structured text can be more efficient for calculations, data handling, and reusable code. The right choice depends on the platform, the application, the site's standards, and the people who will support the system after commissioning.
Industrial communication is another major part of the job. Controllers, drives, barcode readers, robot controllers, and remote I/O need to exchange information reliably. Ethernet-based protocols are common, but compatibility is not automatic. Engineers must understand network layout, addressing, managed switches, device configuration, and the consequences of lost communication.
Cybersecurity now belongs in that conversation as well. Connecting operational technology to business networks can improve visibility and reporting, but it also expands risk. Practical controls design includes access levels, change control, backups, network segmentation, and a recovery plan for failed hardware. A system that cannot be restored after a controller failure is not fully engineered.
Commissioning Is Where Design Meets Reality
Commissioning is the stage that exposes assumptions. Before equipment starts, a controls engineer may perform I/O checks, verify motor rotation, test safety circuits, confirm instrument scaling, and simulate faults. Once the process is live, they refine sequence timing, alarm limits, and operator displays.
This work often happens under difficult constraints. A plant shutdown may last only a weekend. A production line may need to restart before the next shift. Changing logic too quickly can create a new problem, but delaying a needed change can extend downtime. The best engineers stay methodical even when the environment is not calm.
Documentation helps protect that discipline. Electrical schematics, I/O lists, control narratives, network diagrams, PLC backups, and revision records may not feel as satisfying as getting a machine to run. They are still essential. The person troubleshooting a failure at 2 a.m. needs an accurate picture of the system, not a memory of how it was intended to work.
Skills That Make the Role Work
Technical knowledge matters, but the role rewards engineers who can move between detail and context. They need enough electrical understanding to trace a signal, enough programming skill to interpret control logic, and enough process knowledge to recognize when a problem originates outside the code.
Troubleshooting is especially valuable. A useful approach is to separate symptoms from causes. If a conveyor will not start, the issue might be a motor overload, an emergency stop circuit, a missing permissive from downstream equipment, a failed output module, or a networked drive that is not ready. Guessing wastes time. A structured check of power, safety, inputs, logic, outputs, and mechanical conditions narrows the fault quickly.
Communication is equally practical. Controls engineers routinely explain technical decisions to electricians, operators, maintenance technicians, project managers, equipment vendors, and other engineers. A clear alarm message or a well-labeled HMI screen can reduce downtime more effectively than a sophisticated feature that no one understands.
Becoming a Controls Engineer
There is no single path into controls engineering. Many professionals begin with degrees in electrical, mechanical, computer, chemical, or mechatronics engineering. Others build experience through automation technician roles, maintenance work, industrial electrician apprenticeships, or associate programs focused on instrumentation and controls.
For students and early-career professionals, hands-on practice is a strong differentiator. Learn how a sensor is wired, how a relay behaves, how to read a basic electrical schematic, and how a PLC scan cycle affects program behavior. Small training projects can teach meaningful lessons when they include faults, not just ideal operation. Build a sequence, add safety conditions, create alarms, and document how another person would troubleshoot it.
Vendor platforms are common in the field, but platform familiarity alone does not define competence. The transferable skill is understanding control principles: discrete logic, analog signals, sequencing, feedback control, electrical safety, machine safety, and disciplined testing. Specific software can be learned. Sound engineering habits take longer to develop.
Why the Role Continues to Matter
Automation is expanding, but that does not make controls engineering a simple software job. Physical systems still need to be understood, integrated, maintained, and improved. Plants also face pressure to reduce waste, capture better production data, use energy more efficiently, and operate with fewer unplanned interruptions.
That creates opportunity, along with responsibility. More connected systems can provide useful data, yet they can also become harder to support if their design is poorly documented or their alarms are poorly managed. More automation can improve consistency, but only when the system reflects how operators and maintenance teams actually work.
A capable controls engineer brings order to that complexity. Start with the physical process, verify each signal, make failure states understandable, and leave the next person a system they can safely operate. That is the standard worth building toward.